QualiView / SAVI
Protect the product.
Support the inspector.
When the viewing direction moves away, the inspection presentation can pause. QualiView brings camera-based head and gaze-direction estimates into a configured semi-automated visual inspection workflow.
Designed to support the inspection opportunity—not to grade people or declare a product acceptable.
Try the concept
Look away. Hold the presentation.
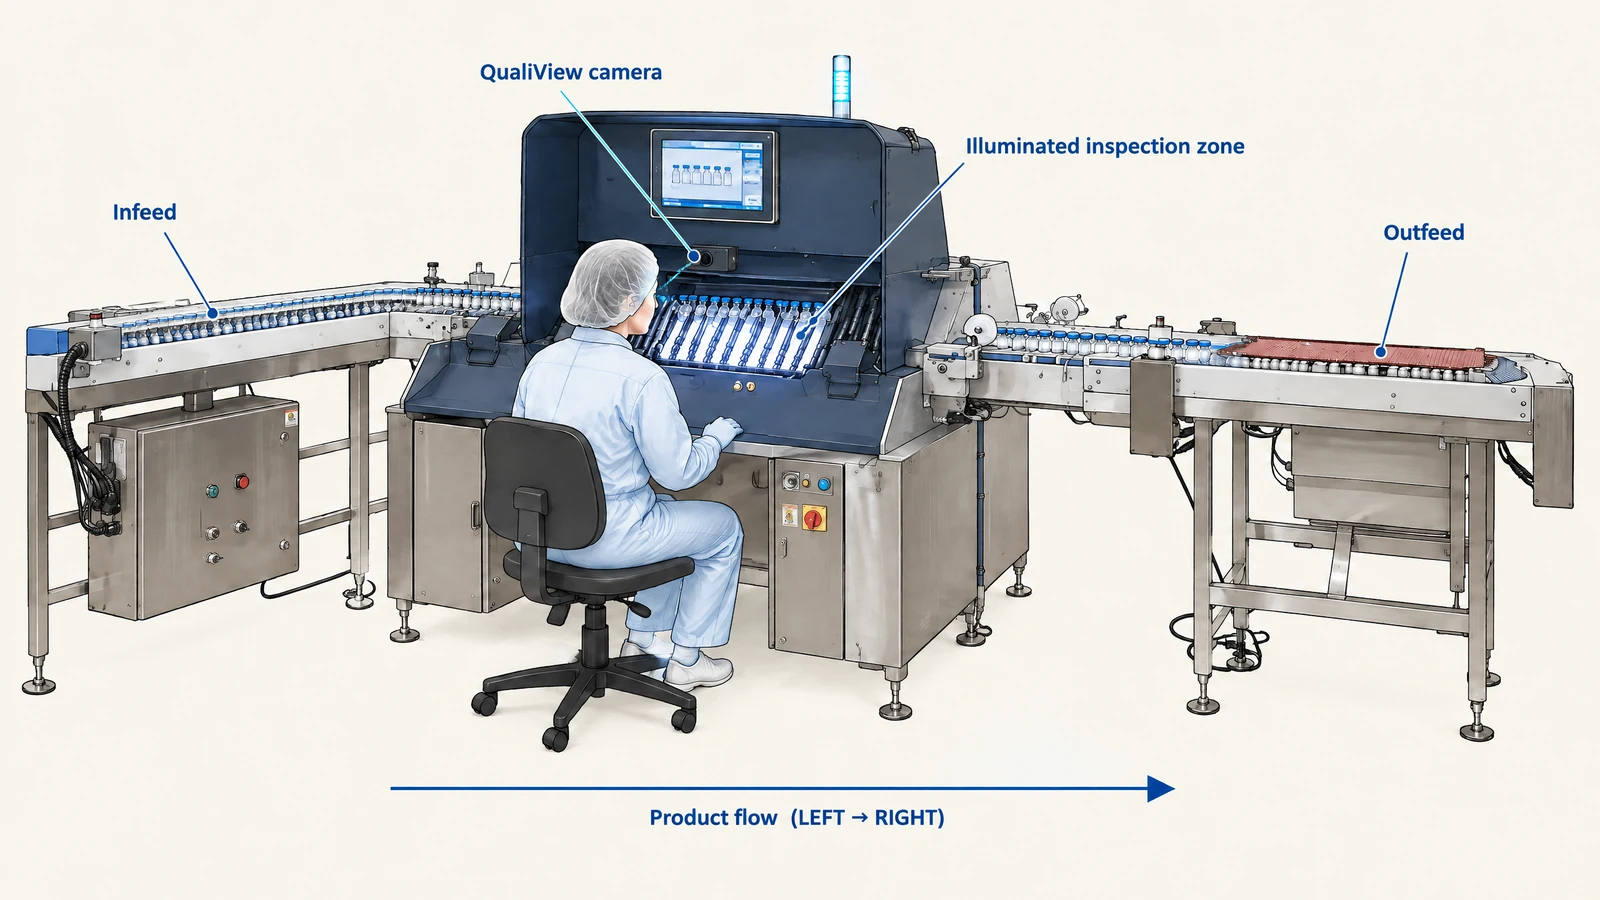
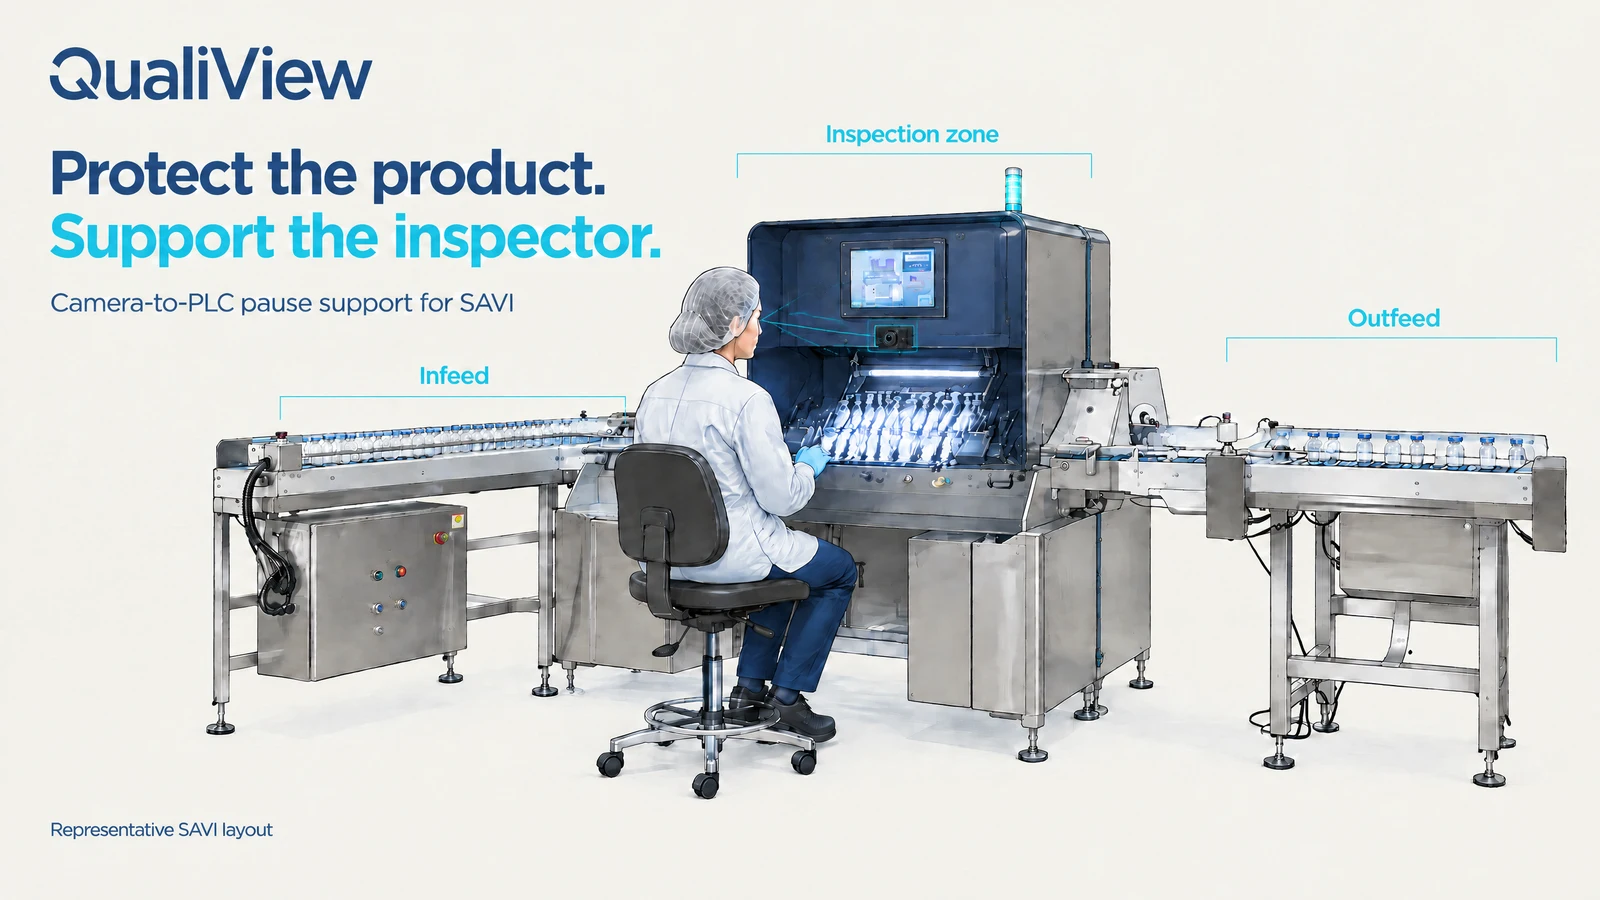
InfeedGeneric transport enters from the left.
Illuminated inspection zoneInclined, roller-supported carriers sit inside the open-front hood.
OutfeedGeneric transport continues to the right.
Camera estimate
Direction toward viewing area
Configured condition
Within illustrated viewing region
PLC interface
No pause request shown
Presentation state
Presentation available
From observation to process control
The camera watches direction.
The inspector examines the product.
In the owner-described SAVI use case, a camera tracks facial features to estimate head and gaze direction. A configured turn-away condition sends a pause request to the programmable logic controller (PLC), which pauses the inspection sequence. The signal does not detect defects.
In a representative conveyor-fed SAVI layout, containers move from the infeed through a controlled, illuminated viewing area to the outfeed. The inspector faces the viewing aperture and examines the presented containers; handling and rotation depend on the system. The QualiView camera is mounted in the inspection viewing area—the same area the inspector looks toward when examining the product. It faces the inspector straight-on along that viewing direction, not from an overhead or side-mounted position, and does not act as a vial defect-detection camera. The diagram shows left-to-right flow for clarity, not a universal machine direction.
- 01
Observe facial features
A camera in the inspection viewing area faces the inspector straight-on; placement is assessed for the actual working position and conditions.
- 02
Estimate viewing direction
Interpret estimates against the defined inspection viewing region—not as a score of cognitive attention.
- 03
Request a PLC pause
Apply the configured turn-away rule through an engineered control-system interface.
- 04
Manage the interruption
Use approved handling and restart rules for the presentation and any affected units.
The product use case is described by the owner and the original YB Systems overview. Installation behavior and performance require project-specific evidence.
Support, not surveillance scoring
Account for human nature.
Do not turn it into blame.
A momentary turn is not a character judgment. Necessary task movements, permitted viewing positions, ergonomics, and breaks belong in the approved workflow. The purpose is to support the opportunity to inspect—not to infer motivation or punish an inspector.
Make that purpose transparent. Agree how camera data will be used, who can access it, and what is retained before deployment. Those privacy and governance arrangements must be confirmed for the actual configuration; this page does not assert undocumented privacy features.
A useful control input.
Not proof of inspection.
Looking toward a vial does not prove a defect was seen. QualiView does not replace trained inspectors, qualified methods, representative challenge sets, appropriate lighting, suitable breaks, or an effective inspection program.
The cited FDA draft, EU Annex 1, and USP materials address inspection capability and controls. They do not prescribe facial tracking as a required inspection measure. Sources and status
Define the use case
Specify the viewing region, permitted task movements, camera/PPE/lighting conditions, signal interpretation, and machine interface.
Challenge the complete workflow
Assess missed look-away conditions and unwanted pauses, signal loss, response latency, overrides, and recovery under representative working conditions. Do not assume a universal angle or delay.
Control affected units and restart
Define what happens to products presented during an interruption, whether reinspection is needed, and who can restart. A pause request is not a reject or release decision.
Keep process control separate from safety
This page describes a process-control pause. It makes no claim of an emergency-stop function, safety-integrity rating, or personnel-protection certification.
A familiar idea. A different qualification task.
If a camera can support the driver,
why not support the inspection process?
Camera-based driver monitoring makes the technology idea familiar. The cited automotive framework addresses distraction warning, not pharmaceutical inspection. It does not transfer automotive thresholds, approvals, or performance evidence to a pharmaceutical inspection line.
Manufacturing needs its own intended-use assessment, integration engineering, qualification, and data governance. No quantified improvement in defect detection, error rate, or productivity is claimed here.
Sources and claim boundaries
Manufacturer descriptions support the stated use case, not a guarantee of performance. The automotive sources are analogies only. Regulatory and compendial status is labeled below; use current applicable texts and approved site procedures for operational decisions.
- QualiView: original YB Systems product overview
Manufacturer description; not product-performance validation evidence
- FDA: Inspection of Injectable Products for Visible Particulates
December 2021 draft guidance; nonbinding, not for implementation
- EU GMP Annex 1: Manufacture of Sterile Medicinal Products
EU GMP guidance; visual inspection context in sections 8.30–8.33
- USP <1790>: Visual Inspection of Injections
Informational compendial chapter; inspection remains probabilistic
- European Commission: advanced driver distraction warning framework
Automotive framework; not a pharmaceutical requirement or equivalence
Build the control around your SAVI process.
Start with your presentation mechanism, inspector position, PLC platform, and approved inspection workflow.